CRANKSHAFT
1. Check crankshaft journals and pins for score, bias, wear or
cracks. If faults are minor, correct with fine crocus cloth.
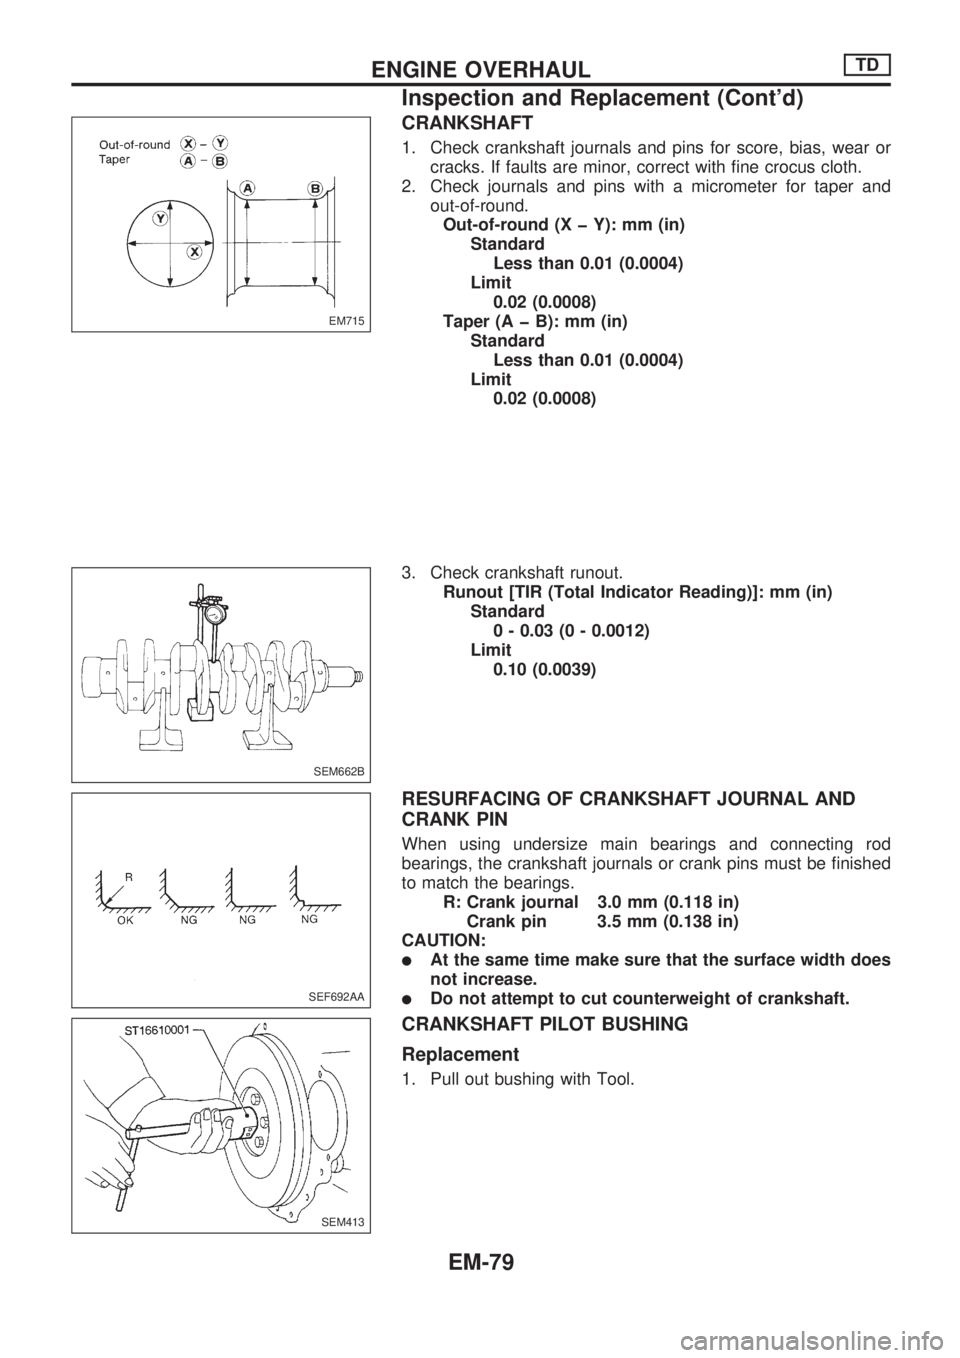
2. Check journals and pins with a micrometer for taper and
out-of-round.
Out-of-round (X þ Y): mm (in)
Standard
Less than 0.01 (0.0004)
Limit
0.02 (0.0008)
Taper (A þ B): mm (in)
Standard
Less than 0.01 (0.0004)
Limit
0.02 (0.0008)
3. Check crankshaft runout.
Runout [TIR (Total Indicator Reading)]: mm (in)
Standard
0 - 0.03 (0 - 0.0012)
Limit
0.10 (0.0039)
RESURFACING OF CRANKSHAFT JOURNAL AND
CRANK PIN
When using undersize main bearings and connecting rod
bearings, the crankshaft journals or crank pins must be finished
to match the bearings.
R: Crank journal 3.0 mm (0.118 in)
Crank pin 3.5 mm (0.138 in)
CAUTION:
lAt the same time make sure that the surface width does
not increase.
lDo not attempt to cut counterweight of crankshaft.
CRANKSHAFT PILOT BUSHING
Replacement
1. Pull out bushing with Tool.
EM715
SEM662B
SEF692AA
SEM413
ENGINE OVERHAULTD
Inspection and Replacement (Cont'd)
EM-79